Beyond the Blueprint: How Precision Gear Machining Ensures 25+ Years of Reliable Operation in Demanding Australian Conditions
Introduction

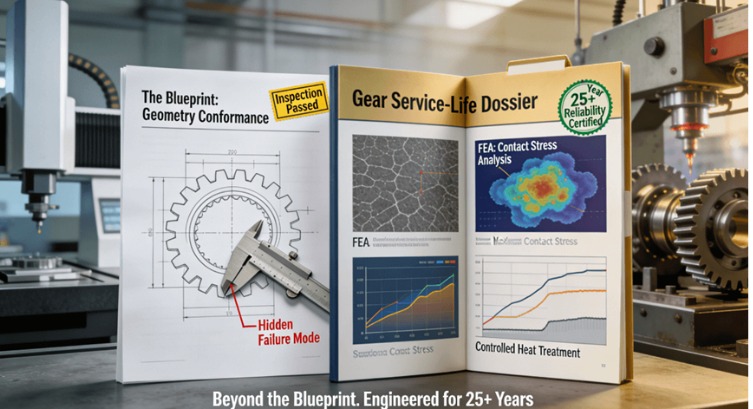
In the mining, agriculture, maritime, and heavy industries of Australia, the cost of an unexpected drivetrain failure is exceptionally high — equipment downtime in remote locations, critical production line stoppages. Engineers often find that even gears manufactured strictly to drawing and passing incoming inspection can fail prematurely under harsh loads, dust, or thermal cycling, succumbing to pitting, tooth breakage, or excessive wear long before their design life. The core problem is that traditional gear procurement often stops at “drawing conformance.” However, what determines 25+ years of service life are factors a drawing cannot fully define: the material’s microstructure, residual stress distribution, the interaction of tooth surface texture with lubrication, and the alignment of heat treatment with the end-use environment. This is a classic “design-manufacture disconnect.”
This article outlines a “Service-Life-Oriented Gear Systems Engineering” methodology. It treats a gear as a complete system under dynamic load, integrating material science, manufacturing process simulation, micro-geometric control, and preventative quality data packages. This transforms long-term gear reliability from a probabilistic hope into a predictable, verifiable engineering output. Let’s explore the four key dimensions of this systems approach and see how it engraves “reliable” into every grain of the metal.
Why Do Gears That Pass Inspection Sometimes Fail Prematurely in the Field?
This section analyzes the critical gap between passing a dimensional inspection and achieving reliable, long-term performance in service, arguing that true reliability is rooted in material and process integrity, not just geometry.
The Dimensional Mirage: Passing the Check, Failing the Test
A gear can pass all pin and CMM checks yet be destined for premature failure. Consider a high-torque gear in a mining reducer. Its failure may not stem from a wrong dimension but from insufficient core hardness, leading to a brittle fracture under shock load, or from subsurface inclusions acting as initiation points for fatigue cracks. These material flaws are invisible to standard metrology but are fatal under cyclic loading. The drawing, as defined by standards like ASME Y14.5, sets the permissible geometric boundaries, but long-term reliability depends on the integrity of the material and process chain that brings that geometry to life.
Performance Over Paper: The Need for “Performance Traceability”
Therefore, quality assurance must extend beyond verifying that “Feature A is within ±0.05mm.” It requires performance traceability — evidence that the material’s chemical composition, cleanliness (e.g., per ASTM E45), and final mechanical properties (hardness, case depth) are suitable for the application’s specific stress spectrum. A gear for a continuously operating conveyor in the Pilbara faces different demands than one in a intermittently used winch, even if the drawings are identical. Assessing a supplier requires looking for this depth of validation.
Building a Holistic View of Quality
This holistic view moves from a checklist mentality to a systems understanding. It acknowledges that a perfect tooth profile is worthless if the underlying material is flawed. To comprehensively master the full chain from design principles to manufacturing processes, and through to cost and quality control, this in-depth guide on gear machining services provides a complete analysis of this complexity.
What Are the True Cost Drivers in Gear Machining? A Transparent Breakdown.
This section deconstructs a gear machining quote into its core, transparent cost drivers, arguing that a clear breakdown is a proxy for supplier competency and the only way to make value-based, rather than price-based, procurement decisions.
Material Cost: Beyond the Price per Kilo
The material line item should specify the exact alloy and grade, the required raw stock size, its cost, and the calculated material utilization percentage. A low utilization rate (e.g., 40%) signals high waste and is a primary target for cost optimization, potentially through design tweaks or blank size reassessment. Transparency here prevents you from overpaying for scrap.
The Manufacturing Process Stack: Time and Technology
A professional quote itemizes the cost of each major process step. This typically includes:
l Primary Machining: Rough turning/gear hobbing or shaping.
l Heat Treatment: Carburizing, quenching, tempering — often a significant cost center.
l Finishing: Gear grinding or honing for precision and surface finish.
l Secondary Operations: Shot peening, deburring, coating.
Each step should have an associated time estimate and rate. This breakdown reveals where value (and cost) is added, allowing for informed discussions about process alternatives.
The Cost of Assurance: Inspection and Documentation
Never view inspection as “free.” A credible gear machining quote will itemize the cost of quality assurance, such as First Article Inspection (FAIR) on a gear measuring center, material certification, and hardness testing. This data package is not an add-on; it is the proof of conformance and your risk mitigation. A low quote that omits these items is transferring the cost and risk of validation back to you, impacting the true CNC machining project cost.
How Can Early Design Collaboration Transform a Good Gear into a Great One?
This section explores the immense value of Design for Manufacturability (DFM) in gear projects, positioning the manufacturer as a collaborative engineering partner who can optimize for performance, cost, and reliability from the outset.
The Power of Proactive Optimization
Early collaboration allows the manufacturing expert to suggest optimizations that the designer, focused on function, may overlook. For example, standardizing fillet radii allows the use of a single, optimal grinding wheel. Specifying a more hardenable steel grade might allow for a shallower case depth to achieve the same core strength, reducing distortion and grinding time. These seemingly small changes, guided by production knowledge, can reduce manufacturing difficulty and cost by 15-30% without compromising — and often enhancing — performance.
Designing for the Entire Process Chain
True DFM considers the entire journey. A design that is easy to machine but impossible to heat treat uniformly is a failure. A collaborative partner will assess the design for hobbing/shaping accessibility, heat treatment distortion predictability, and grinding wheel clearance. This system-aware approach prevents costly late-stage changes and ensures the design is robust for volume production, a key consideration for Australian engineering projects requiring local or resilient supply chains.
The Paradigm Shift: From Vendor to Consultant
This requires a shift from treating the gear shop as a passive “order taker” to engaging them as a manufacturing consultant. The return on this investment in collaboration is a component that is not only cheaper to make but also more reliable, as potential failure modes are designed out with production reality in mind. Therefore, fully unlocking the value of DFM and transforming an optimized design into reality hinges on close collaboration with a precision machining gears expert possessing full-spectrum engineering capabilities.
From One Perfect Sample to a Thousand: How is Consistency Guaranteed?
This section delves into the systems and controls required to scale from a single, hand-tuned perfect prototype to thousands of identical, reliable production parts, emphasizing that consistency is a product of statistical process control, not artisan skill.
The Science of Repetition: Statistical Process Control
Creating one perfect gear is an achievement of engineering. Creating ten thousand is an achievement of statistical process control (SPC). In precision gear manufacturing, SPC is applied to critical characteristics like tooth profile and lead deviation. Control charts track these metrics in real-time during production runs (e.g., grinding), triggering alerts if the process shows signs of drifting. This allows for corrective action beforea single out-of-spec part is produced, ensuring every gear in the batch is a true copy of the first.
The Role of Advanced Metrology and Feedback
This control is enabled by advanced metrology. Gear measuring centers provide exhaustive data that is not just for a pass/fail decision but is fed back into the SPC system. This data, when correlated with process parameters, builds a predictive model of the manufacturing process. Understanding the predictable distortion behavior of specific alloys during heat treatment, as documented in resources like the ASM International Handbook, allows for pre-compensation in machining, making consistency a calculated output.
Systematizing Quality: The Framework of Standards
This data-driven, preventive approach is institutionalized by quality management systems like ISO 9001 and IATF 16949. These standards mandate documented control plans, production part approval processes (PPAP), and rigorous corrective action protocols. For a gear supplier, these certifications are not just plaques; they are a blueprint for achieving and documenting the batch-to-batch consistency that 25-year reliability demands.
What Should You Look for in a Gear Manufacturing Partner Beyond the Machine List?
This final section provides a practical evaluation checklist for selecting a gear manufacturing partner, focusing on engineering depth, data transparency, and systemic reliability over a simple list of machine tools.
- Engineering Dialogue and Problem-Solving Capability: During initial discussions, probe their technical depth. Can they discuss the implications of different material grades on wear resistance versus toughness? Can they explain their approach to minimizing heat treatment distortion for your specific gear geometry? A partner who asks informed questions about your application’s load cycles and environment is thinking about your system’s success, not just filling an order. This depth is central to understanding how gear machining works as an integrated solution.
- Evidence and Data Transparency: Request evidence, not assurances. Ask for a sample inspection report from a past project. It should be comprehensive, showing not just pass/fail but actual error plots for profile and lead. Inquire about their SPC data for key processes. A supplier confident in their process will provide this transparency. This evidence-based approach is the foundation of trust and risk reduction.
- Operational and Systemic Maturity: Assess their project and supply chain management. How do they ensure raw material quality and traceability? What is their protocol for managing engineering changes? A partner with a IATF 16949 certification will have structured approaches like Advanced Product Quality Planning (APQP) and 8D problem-solving, which systematically prevent issues and contain them swiftly if they arise, significantly lowering project risk. This operational maturity ensures they are a reliable component of your manufacturing solutions.
Conclusion
In a market like Australia, where equipment reliability is non-negotiable, excellence in gear manufacturing has evolved from a simple machining task into a specialized discipline integrating materials science, precision engineering, and systematic quality management. By adopting a “Service-Life-Oriented Systems Engineering” methodology and partnering with a manufacturer possessing the corresponding depth and transparency, companies can transform drivetrain components from a potential point of failure into a cornerstone of long-term product competitiveness and sterling reputation.
FAQs
Q: What’s the typical lead time for a custom gear prototype versus a production batch?
A: For a functional prototype requiring new programming, machining, and heat treatment, a lead time of 4-6 weeks is realistic, allowing for thorough engineering review. Production batches depend on complexity and volume but often range from 6-10 weeks. The key is a partner with predictable processes and transparent communication.
Q: How do you ensure corrosion resistance for gears used in marine or coastal Australian environments?
A: It starts with material selection (e.g., 316 stainless, specific bronzes). Surface treatments like high-quality hard anodizing for aluminum or controlled electroless nickel plating for steel are critical. The processes must be meticulously managed to avoid issues like hydrogen embrittlement in high-strength steels.
Q: Can you handle both the gear manufacturing and the heat treatment, or is it outsourced?
A: We manage the entire integrated process chain. For critical gears, we work with a select, certified network of heat treatment specialists under our strict specifications and receive full traceability documentation (furnace charts, atmosphere records). This controlled partnership is part of our vertical quality management.
Q: What information do I need to provide to get the most accurate quote and useful DFM feedback?
A: For optimal results, provide: 1) A 3D CAD model and 2D drawing with full GD&T; 2) Target annual volumes; 3) Detailed operating conditions (load, speed, cycles, environment); 4) Any known failure modes from previous designs. This context enables value engineering.
Q: How is intellectual property protected when sharing gear designs for quotation?
A: Protection begins with a robust, mutually executed Non-Disclosure Agreement (NDA). Files are transferred via encrypted portals, and internal access is strictly controlled. We maintain clear data retention and destruction policies. You can request a summary of our security protocols prior to engagement.
Author Bio
This article is based on deep expertise in high-precision transmission component manufacturing, with a specific focus on longevity challenges in demanding environments. As a global manufacturing partner certified to ISO 9001, IATF 16949, and AS9100D, LS Manufacturing is dedicated to delivering reliable gear solutions — from robust prototypes to consistent volume production — through deep technical collaboration. Submit your gear application requirements and operating conditions today to receive a complimentary “Longevity & Reliability Design Optimization Potential” analysis report.